Community

 es
 ua




Files
3D model format
Stereolithography (.stl)
Total files

Slicer settings
Mesh error check
Netfabb
Support
Lifetime support from Gambody team
Update requests
Available to verified buyers
Model complexity
Standard: balanced printing difficulty and moderate part count with assembly steps.
Model versions
DLP/SLA
Assembly method
Connectors, Glue
Features
- The STL files that this version comprises are pre-supported, hollowed out, and have drain holes where needed;
- You may choose to print the STL files one by one or several at once, depending on the dimensions of your resin 3D printer's build plate;
- When slicing several STL files at once, the attachment layers (Platform Touch Shape) may overlap, but the supports must not come into contact.
FFF/FDM
Assembly method
Connectors, Glue
Features
- Assembly kit includes one lock 18_ge_lock_7S(x1) to attach the figurine's body to legs securely without glue; another lock 21_ge_lock_10H(x3) is needed to secure the parts of the split platform;
- Made with a platform to resemble forest grounds.
DLP/SLA
Assembly method
Connectors, Glue
Features
- Made with a platform to resemble forest grounds
SLS
Assembly method
Connectors, Glue, Solid
Features
- Contains 3 parts: a solid-piece version of Ciri model merged with the platform, and a separate version for display flexibility.
- The assembly parts are connected using specially designed integrated connectors that fit securely into the corresponding slots. Optionally, for added strength and rigidity, the static connections can be glued together.
DLP/SLA
Eco parts
Assembly method
Connectors, Glue
Features
- Made with a platform to resemble forest grounds;
- Contains some hollowed out parts to save resin.
Additional details
Part of diorama
No
Add-on pack available
No
You will get instant access to the STL files of Ciri 3D Printer Files | Assembly after completing your purchase. Simply add the model to your cart and check out using PayPal, credit or debit card, Apple Pay, Google Pay, Alipay, or other available payment methods.
Watch the assembly video for Ciri 3D Printer Files | Assembly, and explore more tutorials, behind-the-scenes content, 3D printing timelapses, and painting guides on the official Gambody YouTube channel.
This 3D Figurine consists of files in StereoLithography (.Stl) format that is optimized for 3D printing.
Before printing the files, we strongly recommend reading the PRINTING DETAILS section.
Ciri 3D Printing Figurine comes in 4 versions for each 3D printer type (FFF/FDM, DLP/SLA and SLS). Files for each version are available for download after the purchase.
Detailed information about this 3D printing figurine is available in the DESCRIPTION section.
Before printing, take a look at Printing Details for recommended settings and tips to achieve better results.
| File name | Size (mm | in) | Size(mb) | Printing Time / Filament | |||
|---|---|---|---|---|---|---|
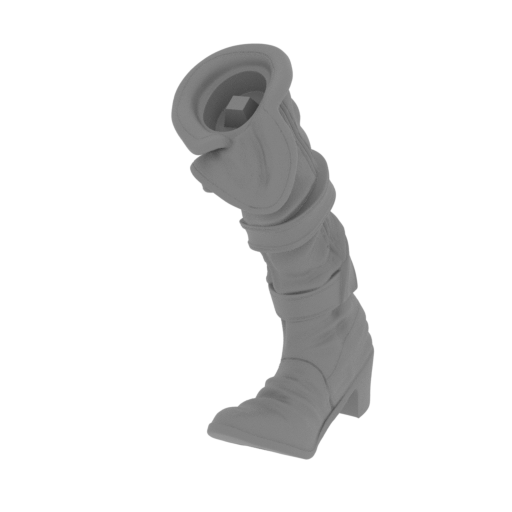 | 10_leg_R_FDM(repaired).stl 33 x 40 x 69 mm | 1.3 x 1.57 x 2.72 in | Size: 33 x 40 x 69 mm | 1.3 x 1.57 x 2.72 in | File size: 21.39 mb | Printing Time / Filament: 1 h 12 min / 4 m Slicer: prusa v2.9.2 Printer: prusa_xl Non default settings Layer height: 0.2 Fill density: 20% Support material: 1 Support material buildplate only: 1 | ||
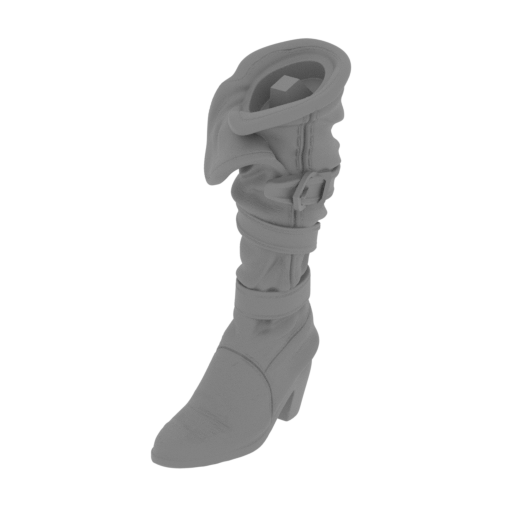 | 9_leg_L_FDM(repaired).stl 28 x 40 x 70 mm | 1.1 x 1.57 x 2.76 in | Size: 28 x 40 x 70 mm | 1.1 x 1.57 x 2.76 in | File size: 18.75 mb | Printing Time / Filament: 1 h 10 min / 4 m Slicer: prusa v2.9.2 Printer: prusa_xl Non default settings Layer height: 0.2 Fill density: 20% Support material: 1 Support material buildplate only: 1 | ||
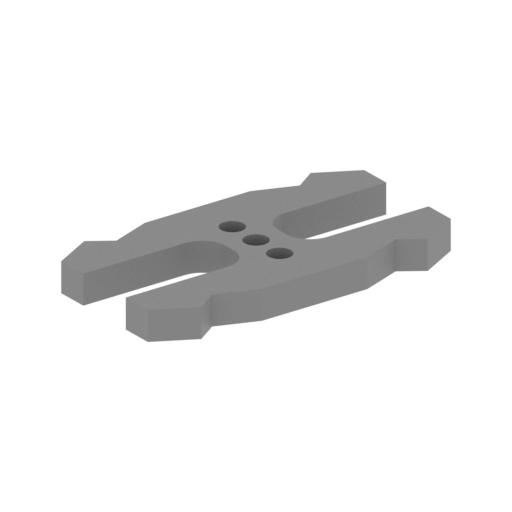 | 21_ge_lock_10H(x3)_FDM.stl 16 x 19 x 2 mm | 0.63 x 0.75 x 0.08 in | Size: 16 x 19 x 2 mm | 0.63 x 0.75 x 0.08 in | File size: 0.03 mb | Printing Time / Filament: 2 min / <1 m Slicer: prusa v2.9.2 Printer: prusa_xl Non default settings Layer height: 0.2 Fill density: 20% Support material: 1 Support material buildplate only: 1 | ||
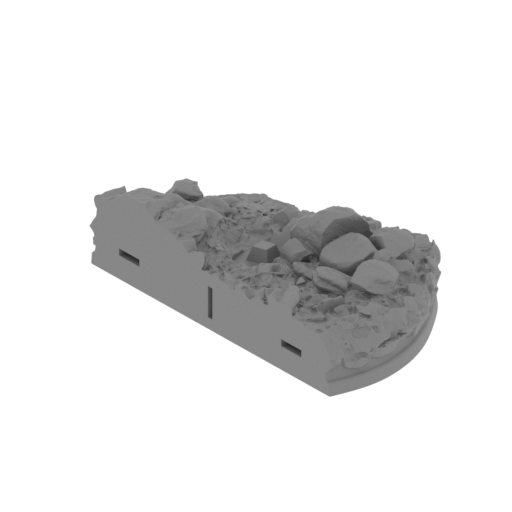 | 20_platform_2_FDM(repaired).stl 112.39 x 99.04 x 33.77 mm | 4.42 x 3.9 x 1.33 in | Size: 112.39 x 99.04 x 33.77 mm | 4.42 x 3.9 x 1.33 in | File size: 30.36 mb | Printing Time / Filament: 2 h 19 min / 15 m Slicer: prusa v2.9.2 Printer: prusa_xl Non default settings Layer height: 0.2 Fill density: 20% Support material: 1 Support material buildplate only: 1 | ||
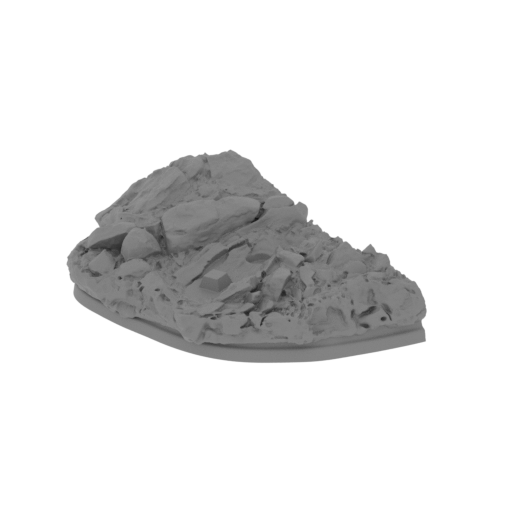 | 19_platform_1_FDM(repaired).stl 119 x 102 x 28 mm | 4.69 x 4.02 x 1.1 in | Size: 119 x 102 x 28 mm | 4.69 x 4.02 x 1.1 in | File size: 28.52 mb | Printing Time / Filament: 2 h 31 min / 16 m Slicer: prusa v2.9.2 Printer: prusa_xl Non default settings Layer height: 0.2 Fill density: 20% Support material: 1 Support material buildplate only: 1 | ||
 | Tag (repaired).stl 150 x 18 x 5 mm | 5.91 x 0.71 x 0.2 in | Size: 150 x 18 x 5 mm | 5.91 x 0.71 x 0.2 in | File size: 1.78 mb | Printing Time / Filament: 18 min / 2 m Slicer: prusa v2.9.2 Printer: prusa_xl Non default settings Layer height: 0.2 Fill density: 20% Support material: 1 Support material buildplate only: 1 | ||
 | Keychain (repaired).stl 30 x 30 x 2 mm | 1.18 x 1.18 x 0.08 in | Size: 30 x 30 x 2 mm | 1.18 x 1.18 x 0.08 in | File size: 0.37 mb | Printing Time / Filament: 6 min / 1 m Slicer: prusa v2.9.2 Printer: prusa_xl Non default settings Layer height: 0.2 Fill density: 20% Support material: 1 Support material buildplate only: 1 | ||
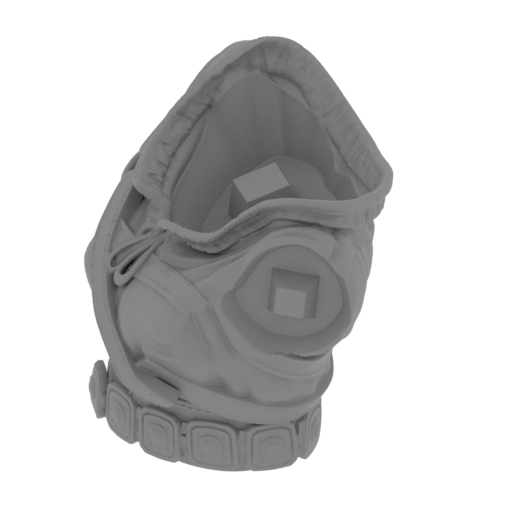 | 3_body_FDM(repaired).stl 47 x 57 x 55 mm | 1.85 x 2.24 x 2.17 in | Size: 47 x 57 x 55 mm | 1.85 x 2.24 x 2.17 in | File size: 32.01 mb | Printing Time / Filament: 1 h 36 min / 8 m Slicer: prusa v2.9.2 Printer: prusa_xl Non default settings Layer height: 0.2 Fill density: 20% Support material: 1 Support material buildplate only: 1 | ||
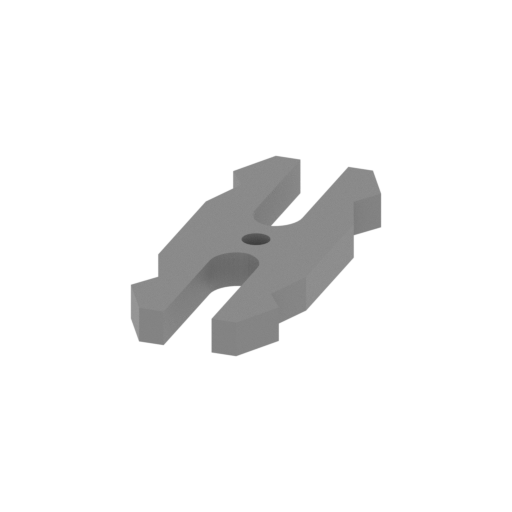 | 18_ge_lock_7S(x1)_FDM(repaired).stl 7 x 18 x 2 mm | 0.28 x 0.71 x 0.08 in | Size: 7 x 18 x 2 mm | 0.28 x 0.71 x 0.08 in | File size: 0.02 mb | Printing Time / Filament: 2 min / <1 m Slicer: prusa v2.9.2 Printer: prusa_xl Non default settings Layer height: 0.2 Fill density: 20% Support material: 1 Support material buildplate only: 1 | ||
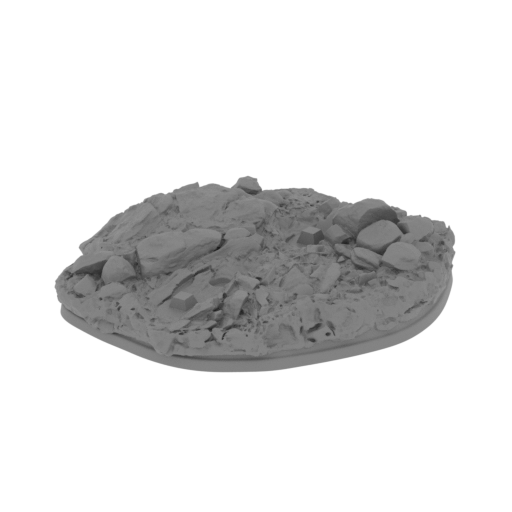 | 17_platform_FDM(repaired).stl 134 x 138 x 34 mm | 5.28 x 5.43 x 1.34 in | Size: 134 x 138 x 34 mm | 5.28 x 5.43 x 1.34 in | File size: 23.35 mb | Printing Time / Filament: 4 h 40 min / 30 m Slicer: prusa v2.9.2 Printer: prusa_xl Non default settings Layer height: 0.2 Fill density: 20% Support material: 1 Support material buildplate only: 1 | ||
 | 16_bag_2_FDM(repaired).stl 17 x 22 x 11 mm | 0.67 x 0.87 x 0.43 in | Size: 17 x 22 x 11 mm | 0.67 x 0.87 x 0.43 in | File size: 14.17 mb | Printing Time / Filament: 9 min / <1 m Slicer: prusa v2.9.2 Printer: prusa_xl Non default settings Layer height: 0.2 Fill density: 20% Support material: 1 Support material buildplate only: 1 | ||
 | 15_bag_1_FDM(repaired).stl 26 x 23 x 13 mm | 1.02 x 0.91 x 0.51 in | Size: 26 x 23 x 13 mm | 1.02 x 0.91 x 0.51 in | File size: 16.74 mb | Printing Time / Filament: 14 min / 1 m Slicer: prusa v2.9.2 Printer: prusa_xl Non default settings Layer height: 0.2 Fill density: 20% Support material: 1 Support material buildplate only: 1 | ||
 | 14_knife_FDM(repaired).stl 8 x 52 x 9 mm | 0.31 x 2.05 x 0.35 in | Size: 8 x 52 x 9 mm | 0.31 x 2.05 x 0.35 in | File size: 9.49 mb | Printing Time / Filament: 7 min / <1 m Slicer: prusa v2.9.2 Printer: prusa_xl Non default settings Layer height: 0.2 Fill density: 20% Support material: 1 Support material buildplate only: 1 | ||
 | 13_sword_3_FDM(repaired).stl 5 x 7 x 12 mm | 0.2 x 0.28 x 0.47 in | Size: 5 x 7 x 12 mm | 0.2 x 0.28 x 0.47 in | File size: 7.79 mb | Printing Time / Filament: 2 min / <1 m Slicer: prusa v2.9.2 Printer: prusa_xl Non default settings Layer height: 0.2 Fill density: 20% Support material: 1 Support material buildplate only: 1 | ||
 | 12_sword_2_FDM(repaired).stl 7 x 7 x 38 mm | 0.28 x 0.28 x 1.5 in | Size: 7 x 7 x 38 mm | 0.28 x 0.28 x 1.5 in | File size: 8.30 mb | Printing Time / Filament: 9 min / <1 m Slicer: prusa v2.9.2 Printer: prusa_xl Non default settings Layer height: 0.2 Fill density: 20% Support material: 1 Support material buildplate only: 1 | ||
 | 11_sword_1_FDM(repaired).stl 142 x 86 x 30 mm | 5.59 x 3.39 x 1.18 in | Size: 142 x 86 x 30 mm | 5.59 x 3.39 x 1.18 in | File size: 18.64 mb | Printing Time / Filament: 23 min / 1 m Slicer: prusa v2.9.2 Printer: prusa_xl Non default settings Layer height: 0.2 Fill density: 20% Support material: 1 Support material buildplate only: 1 | ||
 | 8_hand_L_FDM(repaired).stl 21 x 18 x 44 mm | 0.83 x 0.71 x 1.73 in | Size: 21 x 18 x 44 mm | 0.83 x 0.71 x 1.73 in | File size: 18.47 mb | Printing Time / Filament: 31 min / 1 m Slicer: prusa v2.9.2 Printer: prusa_xl Non default settings Layer height: 0.2 Fill density: 20% Support material: 1 Support material buildplate only: 1 | ||
 | 7_arm_L_FDM(repaired).stl 40 x 28 x 19 mm | 1.57 x 1.1 x 0.75 in | Size: 40 x 28 x 19 mm | 1.57 x 1.1 x 0.75 in | File size: 18.98 mb | Printing Time / Filament: 21 min / 1 m Slicer: prusa v2.9.2 Printer: prusa_xl Non default settings Layer height: 0.2 Fill density: 20% Support material: 1 Support material buildplate only: 1 | ||
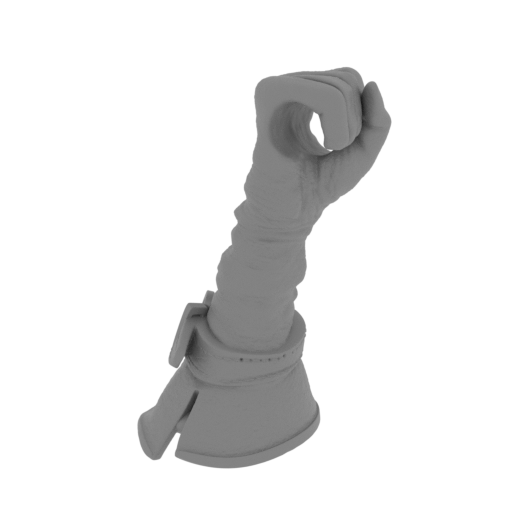 | 6_hand_R_FDM(repaired).stl 23 x 22 x 40 mm | 0.91 x 0.87 x 1.57 in | Size: 23 x 22 x 40 mm | 0.91 x 0.87 x 1.57 in | File size: 20.64 mb | Printing Time / Filament: 34 min / 1 m Slicer: prusa v2.9.2 Printer: prusa_xl Non default settings Layer height: 0.2 Fill density: 20% Support material: 1 Support material buildplate only: 1 | ||
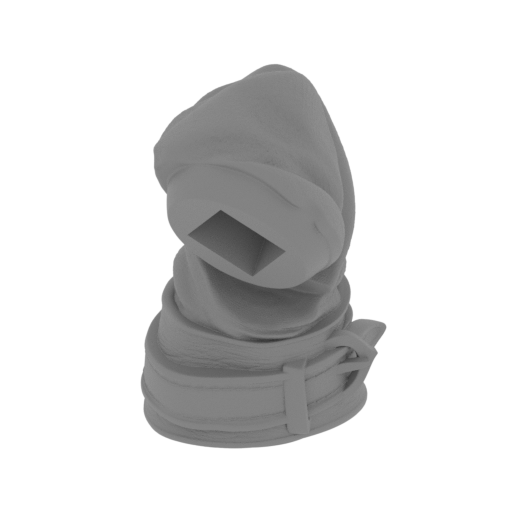 | 5_arm_R_FDM(repaired).stl 18 x 21 x 30 mm | 0.71 x 0.83 x 1.18 in | Size: 18 x 21 x 30 mm | 0.71 x 0.83 x 1.18 in | File size: 16.49 mb | Printing Time / Filament: 27 min / 1 m Slicer: prusa v2.9.2 Printer: prusa_xl Non default settings Layer height: 0.2 Fill density: 20% Support material: 1 Support material buildplate only: 1 | ||
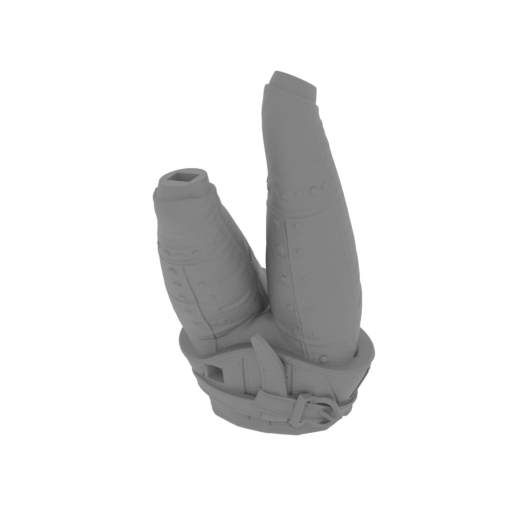 | 4_legs_FDM(repaired).stl 49 x 63 x 95 mm | 1.93 x 2.48 x 3.74 in | Size: 49 x 63 x 95 mm | 1.93 x 2.48 x 3.74 in | File size: 29.94 mb | Printing Time / Filament: 1 h 60 min / 10 m Slicer: prusa v2.9.2 Printer: prusa_xl Non default settings Layer height: 0.2 Fill density: 20% Support material: 1 Support material buildplate only: 1 | ||
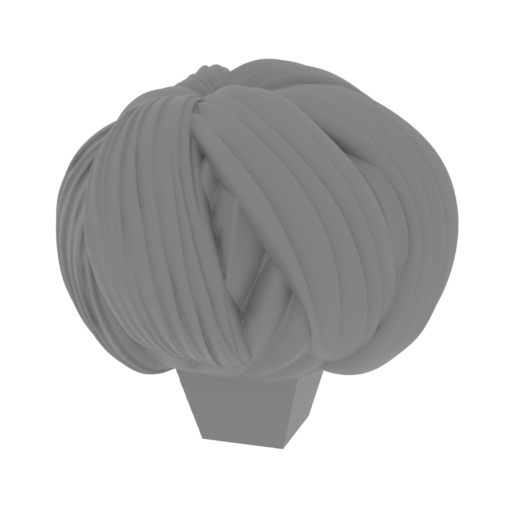 | 2_topknot_FDM(repaired).stl 15 x 14 x 14 mm | 0.59 x 0.55 x 0.55 in | Size: 15 x 14 x 14 mm | 0.59 x 0.55 x 0.55 in | File size: 5.97 mb | Printing Time / Filament: 12 min / <1 m Slicer: prusa v2.9.2 Printer: prusa_xl Non default settings Layer height: 0.2 Fill density: 20% Support material: 1 Support material buildplate only: 1 | ||
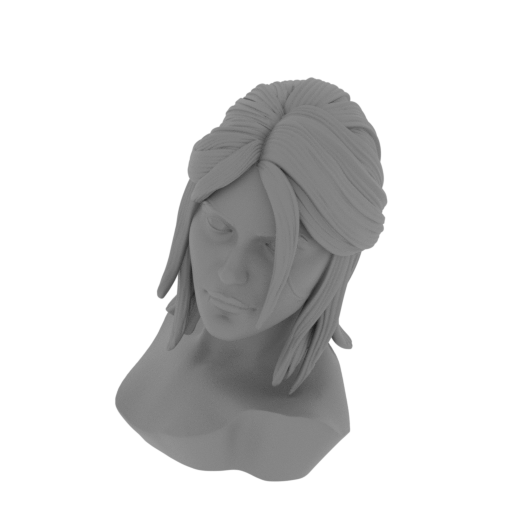 | 1_head_FDM(repaired).stl 33 x 35 x 48 mm | 1.3 x 1.38 x 1.89 in | Size: 33 x 35 x 48 mm | 1.3 x 1.38 x 1.89 in | File size: 27.07 mb | Printing Time / Filament: 59 min / 4 m Slicer: prusa v2.9.2 Printer: prusa_xl Non default settings Layer height: 0.2 Fill density: 20% Support material: 1 Support material buildplate only: 1 | ||
3D model history
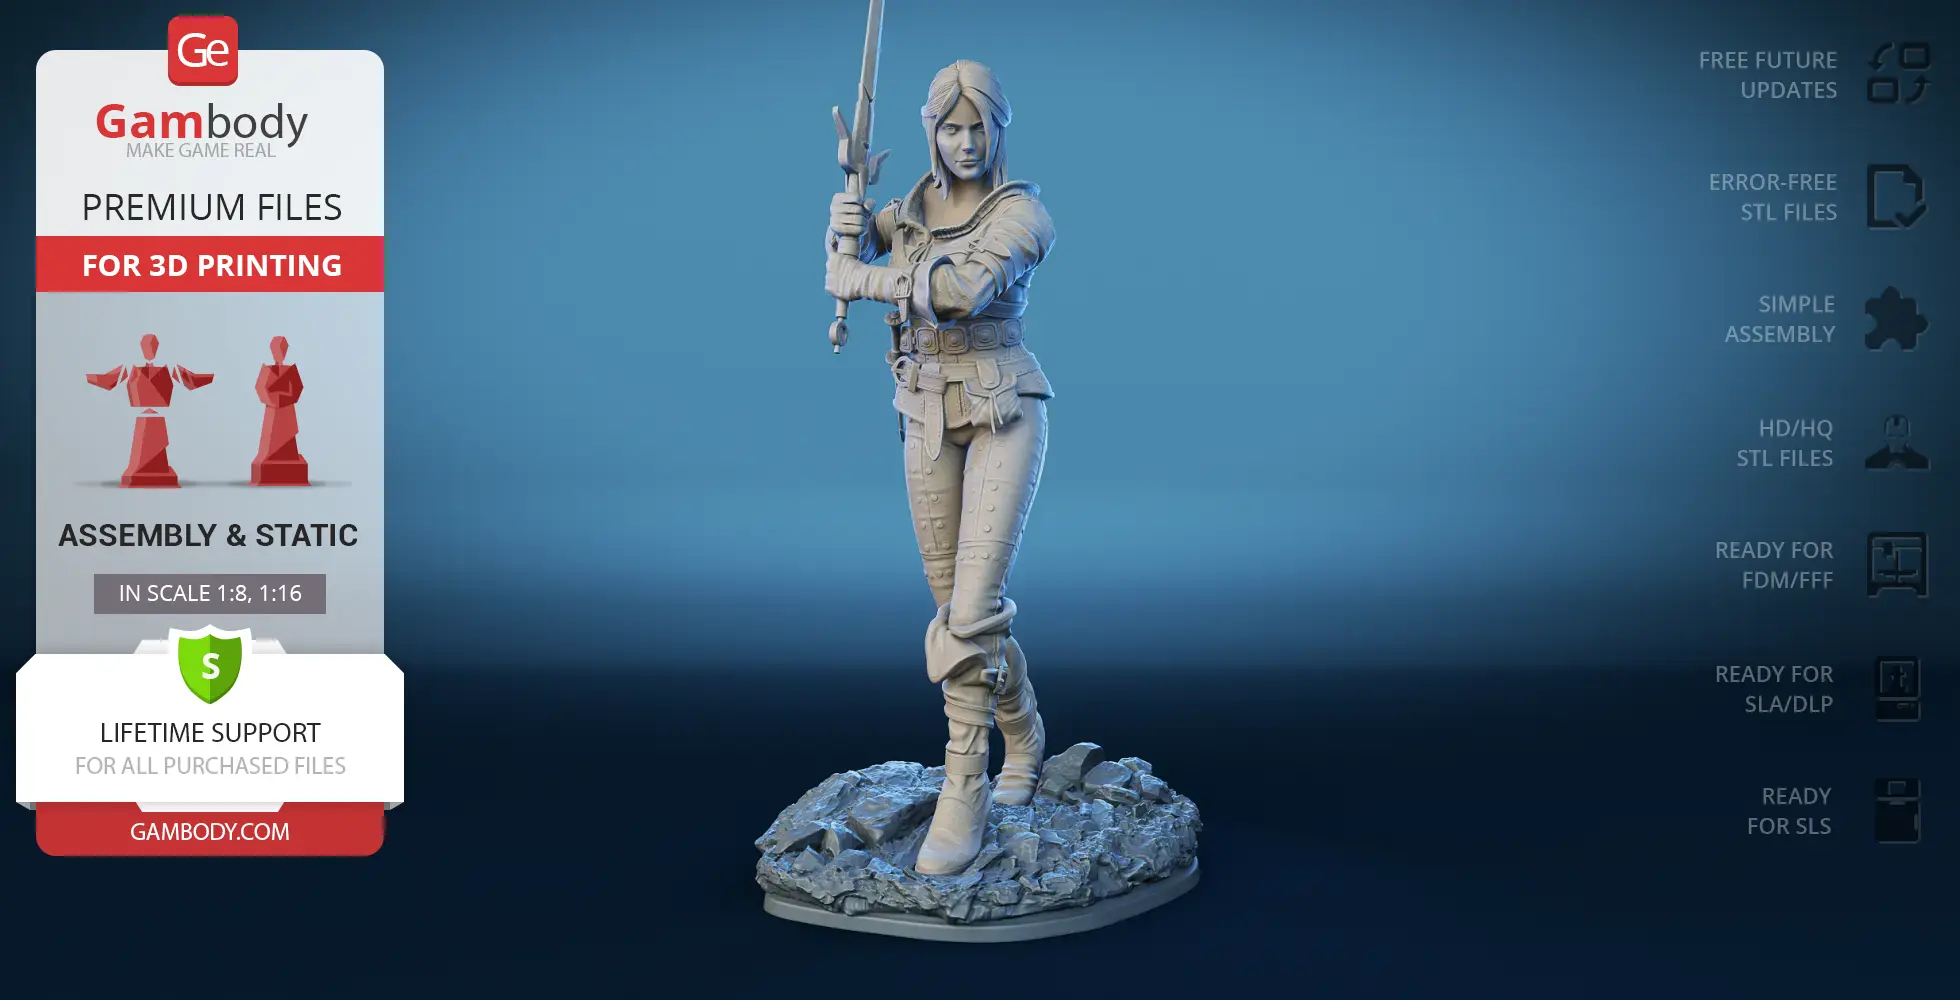
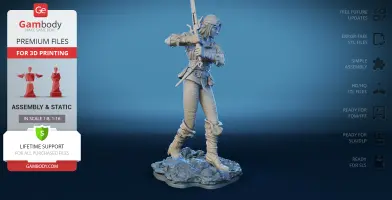
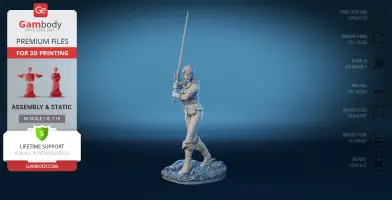
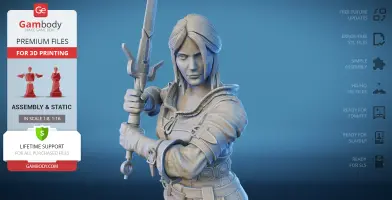
Ciri, whose full name is Cirilla Fiona Elen Riannon, is an adopted daughter of Geralt of Rivia and Yennefer of Vengerberg and one of the main characters within The Witcher novel, video game and television series. Lion Cub of Cintra was born a princess but through tragedy and war, she has come under the care of Geralt of Rivia to become a monster-hunter-in-training. The Witcher, a universe full of wild beasts and fairytale monsters found its passionate fans among fantasy readers, gamers and talented minds of all kinds. Therefore, it is only natural that now every 3D printing enthusiast has a chance to get one’s hands on the beautiful Cirilla model for 3D printing. Thanks to the author of the model, the Lady of Space and Time is portrayed as brave as ever. The sorceress’ stare is determined and her hair is partially pulled back in a loose bun, as if perfectly ready to plunge into a battle. As expected, a deep scar adorns the Ciri’s cheek as a sign of the many confrontations that hardened the princess and perfected her Witcher’s skills. Ciri for 3D printing is also depicted holding a precious gnomish sword called Zireael. That means that the "good" ending of The Witcher 3: Wild Hunt was a particular source of 3D artist’s inspiration – the Ashen one is known to wield the gwyhyr only if survives. We are pretty sure that no matter if you are passionate about the Andrzej Sapkowski’s saga or enjoyed the Witcher story through the role-playing game, a 3D printed Ciri model is a must on your shelf!
3D printing model features
Model-specific features:
- Features Ciri in a dynamic action pose, wielding a sword;
- Comes with a themed display base to resemble forest grounds.
Printing & assembly details:
- Provided as error-free STL files compatible with most 3D printers;
- Optimized part division minimizes support material and ensures smooth and precise surface detailing;
- The assembly parts in the FFF/FDM version come in the recommended print orientations for easy bed placement;
- Assembly manual in PDF and video formats is included for the FFF/FDM and DLP/SLA versions;
- The model is available in recommended scales – 1:8 for the FFF/FDM version and 1:16 for the DLP/SLA/SLS versions.
What will you get after purchase?
- 5 versions of Ciri STL files for FFF/FDM, DLP/SLA, DLP/SLA Eco, and SLS – files for all versions are available for download after the purchase;
- STL files of high-poly Ciri model for 3D printing consist of 51 files;
- Sizes for:
- FFF/FDM Model Size: 71 mm wide, 346 mm high, 104 mm deep;
- FFF/FDM Platform Size: 134 mm wide, 34 mm high, 138 mm deep;
- DLP/SLA/SLS Model Size: 36 mm wide, 173 mm high, 52 mm deep;
- DLP/SLA/SLS Platform Size: 67 mm wide, 17 mm high, 69 mm deep;
- Assembly Manual for FFF/FDM and DLP/SLA versions in PDF and video formats;
- Detailed settings that we provide as a recommendation for Bambu Studio, Cura, Orca Slicer, PrusaSlicer, Simplify3D, and Slic3r for the best print;
- Full technical support from the Gambody Support Team.
Average customer rating (13 reviews)
4.9
Ratings breakdown
Click a star rating to filter reviews
Overall experience
Level of detail in the model
4.9
Model cut quality and assembly guide
4.9
Clarity and accuracy of the model page
4.9


 Verified purchase
Level of detail in the model
5
Model cut quality and assembly guide
5
Clarity and accuracy of the model page
5
 This feedback is from a user who hasn't purchased this model
Level of detail in the model
5
Model cut quality and assembly guide
5
Clarity and accuracy of the model page
5
 This feedback is from a user who hasn't purchased this model
Level of detail in the model
5
Model cut quality and assembly guide
5
Clarity and accuracy of the model page
5
This feedback is from a user who hasn't purchased this model Level of detail in the model
5
Model cut quality and assembly guide
5
Clarity and accuracy of the model page
5
Verified purchase Level of detail in the model
5
Model cut quality and assembly guide
5
Clarity and accuracy of the model page
5
Verified purchase Level of detail in the model
5
Model cut quality and assembly guide
5
Clarity and accuracy of the model page
5
Verified purchase Level of detail in the model
5
Model cut quality and assembly guide
5
Clarity and accuracy of the model page
5
This feedback is from a user who hasn't purchased this model Level of detail in the model
5
Model cut quality and assembly guide
5
Clarity and accuracy of the model page
5
Verified purchase Level of detail in the model
5
Model cut quality and assembly guide
5
Clarity and accuracy of the model page
5
This feedback is from a user who hasn't purchased this model Level of detail in the model
4
Model cut quality and assembly guide
4
Clarity and accuracy of the model page
4
 Verified purchase
Level of detail in the model
5
Model cut quality and assembly guide
5
Clarity and accuracy of the model page
5
 This feedback is from a user who hasn't purchased this model
Level of detail in the model
5
Model cut quality and assembly guide
5
Clarity and accuracy of the model page
5

 Community Support Team
Level of detail in the model
5
Model cut quality and assembly guide
5
Clarity and accuracy of the model page
5
Below you'll find detailed slicing settings for Bambu Studio 2.0+, Orca Slicer 2.0+, UltiMaker Cura 5.0+, PrusaSlicer 2.0+, Slic3r 1.3+, Simplify3D 5.0+ to help you get the best results when printing this model. These settings are optimized specifically for this 3D model, but please note they may need slight adjustments depending on your printer or filament. When in doubt, refer to your printer's user manual.
To avoid printing issues and achieve the best quality, we highly recommend applying the following settings:
 Bambu Studio 2.0+
For better quality use 0.12 mm layer height, for fast printing use 0.2 mm layer height. For pins and the Ge connectors, use 0.2 layer height.
120-150% of your Layer Height
But you can paint the seam if you want.
You have to calibrate this parameter
You have to calibrate this parameter
You have to calibrate this parameter
For pins and power elements of the structure, such as the vehicle frame, use 3 loop
Disabled for vehicles and enabled for characters
For 0,2 Layer Height
The parameters in this tab vary greatly, it all depends on the quality of your printer. For example, if you have a classic Ender3, stick to the minimum parameters, but if you have a newer printer, for example Anycubic cobra 3 v2, you can select the maximum recommended values
Settings for advanced users, change these parameters only if you have sufficient 3D printing expertise
Enable this parameter if your model requires supports
We also recommend placing and removing supports manually in some places using special button
1-2 loops for more thick support
Top Z distance = 1-1.3 layer Height. If the supports are hard to remove, try increasing this setting by 0.1-0,4 mm
Bottom Z distance = 1-1.3 layer Height. If the supports are hard to remove, try increasing this setting by 0.1-0,4 mm
You have to calibrate this parameter which one is better for your filament
Increase this parameter if the supports are hard to remove from walls
For PLA and PETG filament types
5-8 mm is optional for small prints that have bad adhesion to the build plate
You have to calibrate this parameter
Read the description on your filament roll
Read the description on your filament roll and increase this parameter for fast printers
Read the description on your filament roll and increase this parameter for fast printers
 Orca Slicer 2.0+
For better quality use 0.12 mm layer height, for fast printing use 0.2 mm layer height. For pins and the Ge connectors, use 0.2 layer height.
120-150% of your Layer Height
But you can paint the seam if you want.
0.01-0.05 You have to calibrate this parameter
0.01-0.05 You have to calibrate this parameter
0.1-0.2 You have to calibrate this parameter
For pins and power elements of the structure, such as the vehicle frame, use 3 loop
Disabled for vehicles and ships, enabled for characters
For 0,2 Layer Height
For 0,2 Layer Height
The parameters in this tab vary greatly, it all depends on the quality of your printer. For example, if you have a classic Ender3, stick to the minimum parameters, but if you have a newer printer, for example, Anycubic Kobra 3 Or Bambulab A1, you can select the maximum recommended values.
Settings for advanced users, change these parameters only if you have sufficient 3D printing expertise
Enable this parameter if your model requires supports
We also recommend placing and removing supports manually in some places using special button
Top Z distance = 1-1.3 layer Height. If the supports are hard to remove, try increasing this setting by 0.1-0,4 mm
Bottom Z distance = 1-1.3 layer Height. If the supports are hard to remove, try increasing this setting by 0.1-0,4 mm
Increase this parameter if the supports are hard to remove from walls
For PLA and PETG filament types
5-8 mm is optional for small prints that have bad adhesion to the build plate
Read the description on your filament roll
Read the description on your filament roll and increase this parameter for fast printers
You have to calibrate this parameter
Read the description on your filament roll and increase this parameter for fast printers
Read the description on your filament roll
This field is filled in according to your printer specifications when you add it to the slicer.
You can add custom G-code here for the start and end of the print. However, be careful - this is for advanced users only!
You have to calibrate your printer using Ge retraction test models
Retraction Length: For direct-drive setups use 0.5 mm to 2.5 mm; for Bowden extruders use 5 to 7 mm
This is how fast the filament is pulled back—40-60 mm/s for direct drive and 30-50 mm/s for Bowden setups.
You have to calibrate this parameter: Reduce it until the printer starts to hit the parts with the nozzle during printing, then increase it by 0.2.
 UltiMaker Cura 5.0+
For better quality use 0.12 mm layer height, for fast printing use 0.2 mm layer height. For pins and the Ge connectors, use 0.2 layer height.
120-150% of your Layer Height
To increase the strength of the print parts, use wall line count: 3
For pins and connectors use 50% Infill
These parameters are for standard PLA plastic. If you are using a different type of plastic, check the printing temperature recommended by the manufacturer. Also, read the description on your filament spool. For fast printers, add +30 °C to the current parameters.
The parameters in this tab vary greatly, it all depends on the quality of your printer. For example, if you have a classic Ender3, stick to the minimum parameters, but if you have a newer printer, for example Anycubic cobra 3 v3, you can select the maximum recommended values
Settings for advanced users, change these parameters only if you have sufficient 3D printing expertise.
You need to calibrate this parameter using Gambody test models. These values are average values for a Direct Drive extruder; for a Bowden extruder, the values should be increased.
You need to calibrate this parameter using Gambody test models. These values are average values for a Direct Drive extruder; for a Bowden extruder, the values should be increased.
Use this value other than 0 if your nozzle catches on the internal infill during travel moves. Try to keep this value as low as possible in height.
Use normal supports to support large, straight surfaces (most mechanical or technical parts).
You have to calibrate this parameter according to the capabilities of your printer and your filament, using a Gambody test models.
Use 1 instead of 0 if your supports are thin and tall. They will be harder to remove, but much stronger.
Top Z distance = 1-1.3 layer Height. If the supports are hard to remove, try increasing this setting by 0.1-0,4 mm
Increase this parameter if the supports are hard to remove from walls
Use tree supports to support complex objects, such as characters.
You have to calibrate this parameter according to the capabilities of your printer and your filament, using a Gambody test models.
Top Z distance = 1-1.3 layer Height. If the supports are hard to remove, try increasing this setting by 0.1-0,4 mm
Increase this parameter if the supports are hard to remove from walls
Use a skirt for all parts when printing on outdated printers.
Use a brim when printing thin but tall parts, as well as parts with a small bed adhesion area.
 PrusaSlicer 2.0+
For better quality use 0.12 mm layer height, for fast printing use 0.2 mm layer height. For pins and the Ge connectors, use 0.2 layer height.
120-150% of your Layer Height
for 0.2 Layer Height
But you can paint the seam if you want.
(for PLA and PETG)
(5-8 mm is optional for small prints that have bad adhesion to the build plate)
Enable this parameter if your model requires supports
(45-50 degree)You have to calibrate this parameter according to the capabilities of your printer
and your filament, using a Gambody test models.
Top contact Z distance = 1-1.3 layer Height. If the supports are hard to remove, try
increasing this setting by 0.1-0,4 mm
Top contact Z distance = 1-1.3 layer Height. If the supports are hard to remove, try
increasing this setting by 0.1-0,4 mm
Increase this parameter if the supports are hard to remove from walls
The parameters in this tab vary greatly, it all depends on the quality of your printer. For example, if you have a classic Ender3, stick to the minimum parameters, but if you have a newer printer, for example Anycubic cobra 3 v3, you can select the maximum recommended values
Settings for advanced users, change these parameters only if you have sufficient 3D printing expertise. Use the minimum value for outdated printers without acceleration calibration, and the maximum value for modern printers if you need it.
These settings only work for 3D printers with multiple extruders
You can try setting all parameters in this section, except the First layer, to values between 0.75% of your nozzle diameter and 1.25% of your nozzle diameter. Adjusting them will help you work out the optimal parameters for the best quality for your print. As for the First layer, you can set it to 150% of the diameter of your nozzle for better adhesion to the build plate (for a nozzle with a diameter of 0.4 mm, the First layer extrusion width can be from 0.3 mm to 0.5 mm)
For better printing quality you have to calibrate this parameter using Gambody test model.
Check your filament manufacturer's temperature recommendations on the spool.
Cooling parameters depends on the material you use for printing.
*for PLA
 Slic3r 1.3+
For better quality use 0.12 mm layer height, for fast printing use 0.2 mm layer height. For pins and the Ge connectors, use 0.2 layer height.
120-150% of your Layer Height
For 0.12 Layer Height
For 0.12 Layer Height
For pins and connectors use 50% Infill
Use skirt for outdated 3d printers
(5-8 mm is optional for small prints that have bad adhesion to the build plate)
Enable this parameter if your model requires supports
(45-60 degree)You have to calibrate this parameter according to the capabilities of your printer and your filament, using a Gambody test models
Contact Z distance = 1-1.3 layer Height. If the supports are hard to remove, try increasing this setting by 0.1-0,4 mm
The parameters in this tab vary greatly, it all depends on the quality of your printer. For example, if you have a classic Ender3, stick to the minimum parameters, but if you have a newer printer, for example Anycubic cobra 3 v3, you can select the maximum recommended values
Settings for advanced users, change these parameters only if you have sufficient 3D printing expertise. Use the minimum value for outdated printers without acceleration calibration, and the maximum value for modern printers if you need it.
You have to calibrate this parameter from 0.9 to 1.1 according to the capabilities of your printer and your filament, using a Gambody test models.
Check your filament manufacturer's temperature recommendations on the spool.
Cooling parameters depends on the material you use for printing.
Calibrate this value if you need to reduce or improve the adhesion between the plastic and the heat bed
Your current nozzle diameter
You need to calibrate this parameter using Gambody test models. These values are average values for a Direct Drive extruder; for a Bowden extruder, the values should be increased.
 Simplify3D 5.0+
Your current nozzle diameter
You have to calibrate this parameter using Gambody test models.
You need to calibrate this parameter using Gambody test models. These values are average values for a Direct Drive extruder; for a Bowden extruder, the values should be increased.
For better quality use 0.12 mm layer height, for fast printing use 0.2 mm layer height. For pins and the Ge connectors, use 0.2 layer height.
For 0,2 Layer Height
For 0,2 Layer Height
To increase the strength of the print parts, use Outline Perimeters: 3
You can enable this parameter to print rounded or spherical models, as well as character models.
Use this option only if your parts are too tight. but better calibrate your printer extrusion
Use this option only if your parts are too tight. but better calibrate your printer extrusion
Use 2 and more if you want to create skirt instead brim
1-2 for skirt and 10-20 for brim
Use for wipe nozzle if you need
Use For ABS filament
For pins and connectors use 50% Infill
Top Z distance = 1-1.3 layer Height. If the supports are hard to remove, try increasing this setting by 0.1-0,4 mm
Calibrate your filament and detect optimal temperature for it
Average temperature for PLA filament
The parameters in this tab vary greatly, it all depends on the quality of your printer. For example, if you have a classic Ender3, stick to the minimum parameters, but if you have a newer printer, for example Anycubic cobra 3 v3, you can select the maximum recommended values
Settings for advanced users, change these parameters only if you have sufficient 3D printing expertise.
DLP/SLA
- The STL files that this version comprises are pre-supported, hollowed out, and have drain holes where needed;
- You may choose to print the STL files one by one or several at once, depending on the dimensions of your resin 3D printer's build plate;
- When slicing several STL files at once, the attachment layers (Platform Touch Shape) may overlap, but the supports must not come into contact.
SLS
- Contains 3 parts: a solid-piece version of Ciri model merged with the platform, and a separate version for display flexibility.
- The assembly parts are connected using specially designed integrated connectors that fit securely into the corresponding slots. Optionally, for added strength and rigidity, the static connections can be glued together.
DLP/SLA
- Made with a platform to resemble forest grounds;
- Contains some hollowed out parts to save resin.
DLP/SLA
- Made with a platform to resemble forest grounds
FFF/FDM
- Assembly kit includes one lock 18_ge_lock_7S(x1) to attach the figurine's body to legs securely without glue; another lock 21_ge_lock_10H(x3) is needed to secure the parts of the split platform;
- Made with a platform to resemble forest grounds.